Insitu Crankshaft Grinding Machine – RA Power Solutions

For nearly five decades, RA Power Solutions has led the industry in portable crankshaft grinding, enabling repair directly on vessels or in power plants—eliminating the need to dismantle or transport heavy engine components.

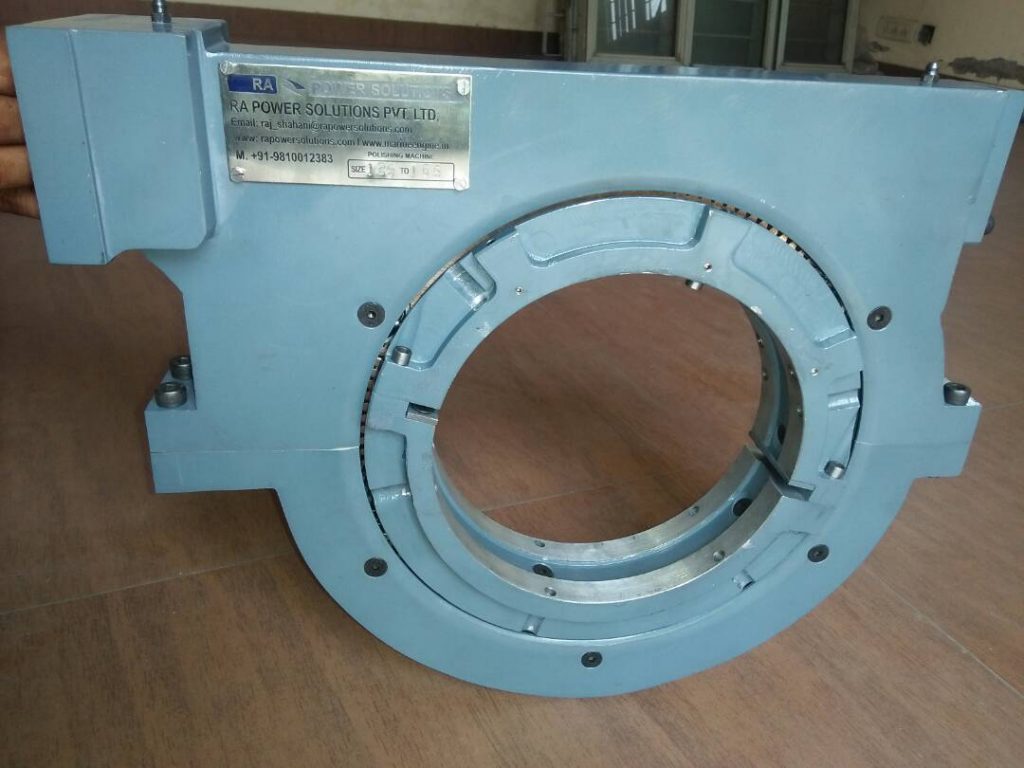
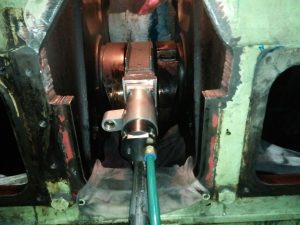
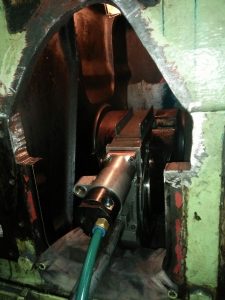
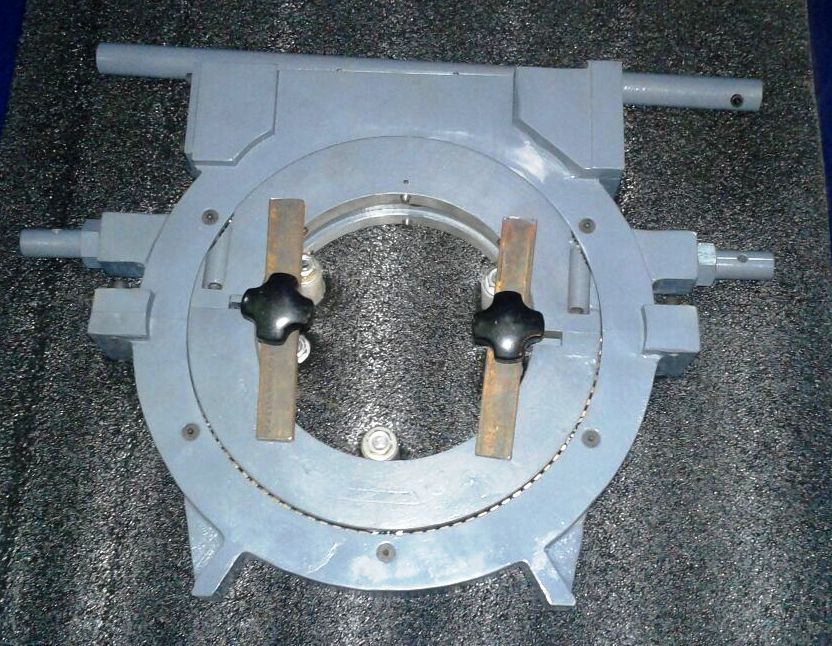
RA Power Solutions manufactures the insitu crankshaft grinding machine, which is lightweight, portable, and easy to operate. We developed and manufactured this revolutionary equipment.

 Globally Deployed Machines & Capabilities:

  • Designed for crankpin and main journal diameters between 35 mm and 700 mm—covering most diesel engine builds
  • We have sold over 100 machines worldwide to shipping firms, power plants, and engine workshops. Clients are located in countries like Singapore, Nigeria, Italy, Saudi Arabia, and beyond.
  • Combines grinding and polishing in one setup, with minimal vibration, maintaining tolerances as tight as 0.02 mm.
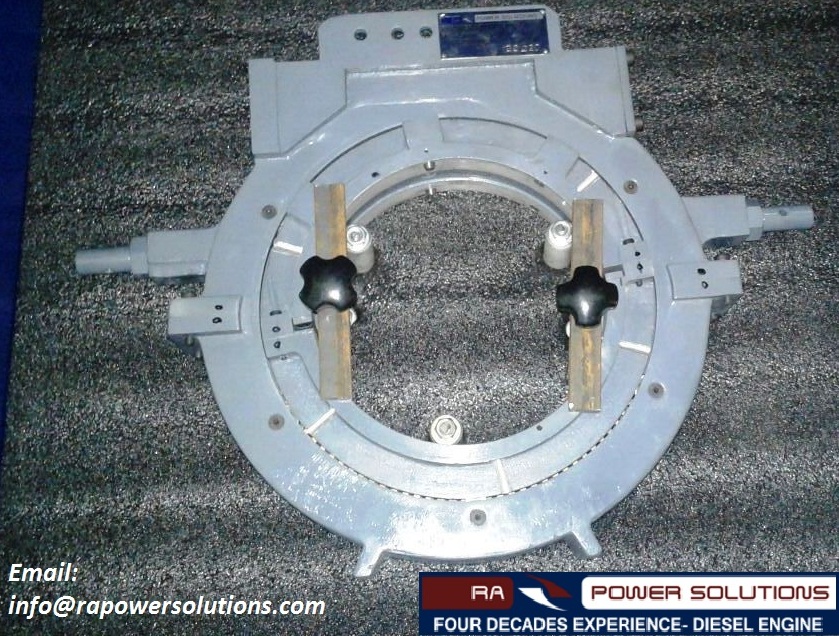
Onsite Crankshaft Grinding Machine

Key Features & Benefits:

FeatureBenefit
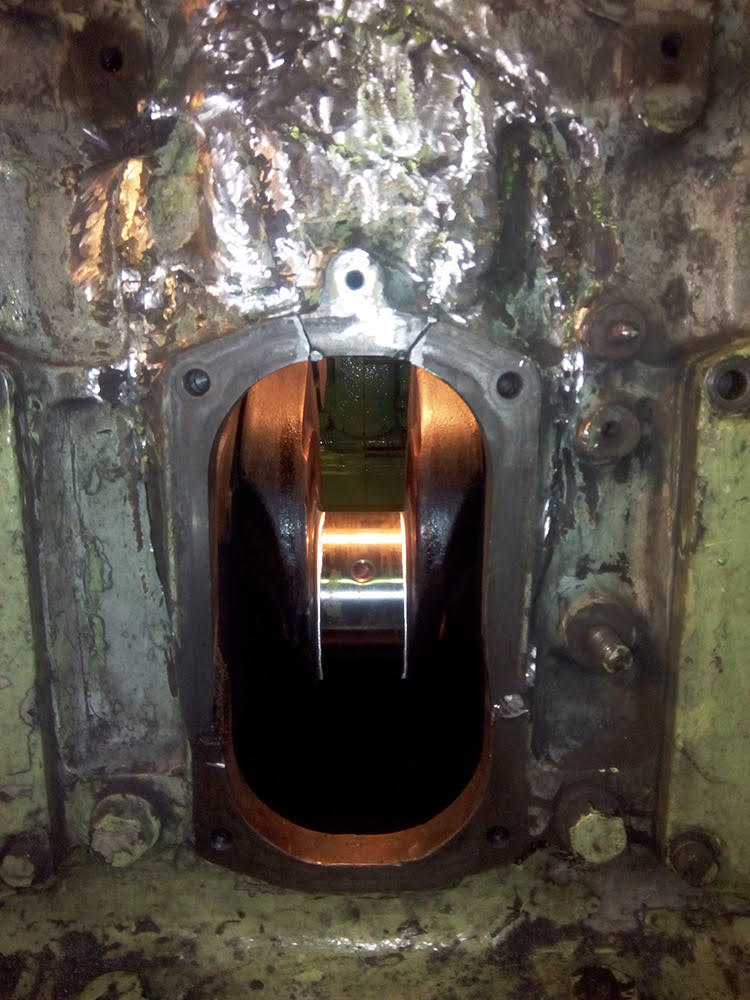
Compact, lightweight designEasily fits through engine inspection windows and transports globally with ease
Titanium‑steel vibration‑absorbing frameEnables grinding even while the vessel is underway, preserving OEM tolerances
Electrical or pneumatic drivesVersatile operation adapted to client’s power infrastructure
On-job training includedTechnicians learn how to operate and maintain the equipment directly from RA Power staff
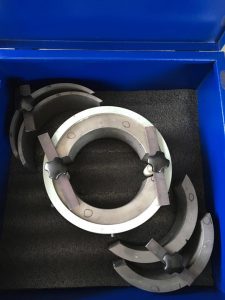
Fully portable toolbox unitSupplied ready-to-use in a steel box—ideal for rapid site deployment

Why Onsite Grinding Beats Workshop Repairs?

  • Reduces downtime by eliminating dismantling and logistics
  • Cuts costs significantly versus sending crankshafts to external workshops
  • Meets or exceeds OEM specifications, including taper, ovality, and surface finish.
    Fully class-approved repair methods and international case studies support machine reliability worldwide.

Proven Track Record

  • RA Power Solutions’ patented handheld machines have repaired over 10,000 crankshafts worldwide, delivering results trusted by shipowners and industrial clients alike.
  • Ideal for marine engines, power-plant diesels, turbines, alternators, and general rotary equipment requiring precision journal repairs.
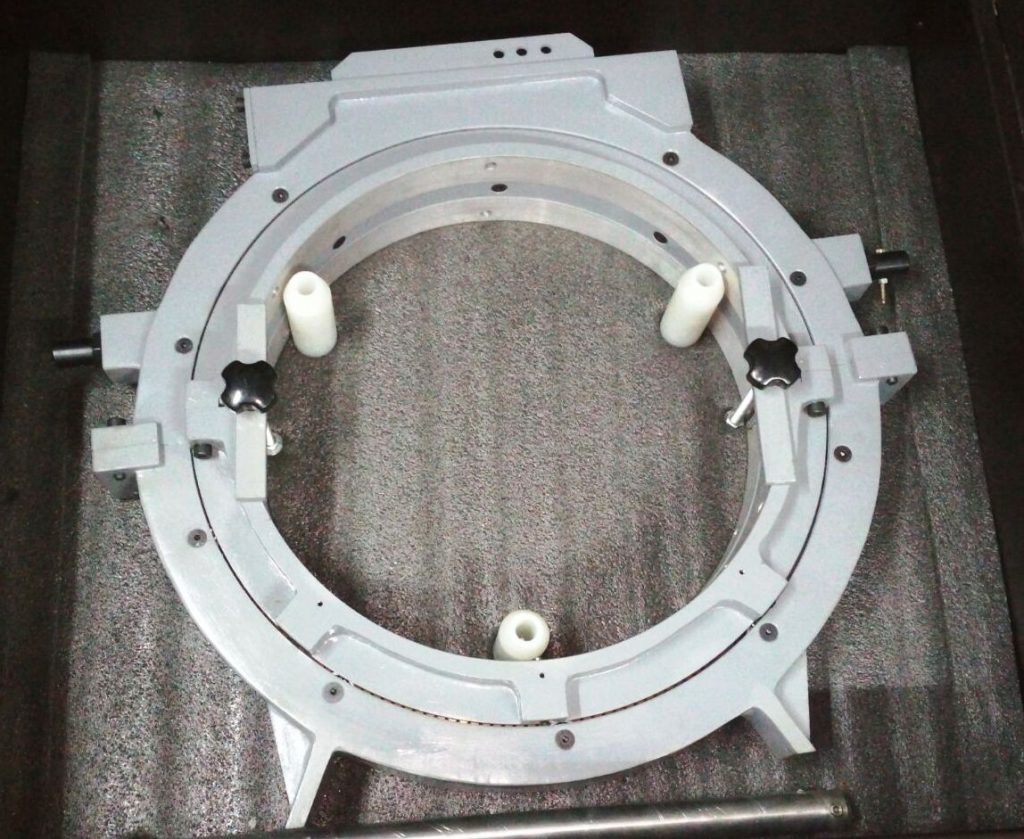
Crankshaft Grinding Machine
Crankshaft Grinder
Crankshaft Grinder

Get in Touch
Need emergency crankshaft repair or onsite polishing? RA Power Solutions offers Insitu Crankshaft Grinding Machine for 24/7 global service with immediate dispatch. Contact us:
Email: rajshahani@rapowersolutions.com or info@rapowersolutions.com

Phone: +91 9582647131 | +91 9810012383

FAQs:

Q1: What is an in-situ crankshaft grinding machine?

Technicians use this portable machine to grind crankshaft journals directly on-site. It eliminates the need to dismantle the engine.

Q2: What crankshaft sizes can your machine handle?

Our machines cover crankpins and main journals ranging from 35 mm to 700 mm in diameter.

Q3: Can the machine be used onboard ships?

The compact, vibration-free design allows technicians to use it on ships—even during voyages.

Q4: What power options are available?

Machines can be operated with either pneumatic or electric power, depending on site conditions.

Q5: Do you provide training with the machine?

Yes, onsite training and support are included to ensure proper operation and maintenance.

For nearly five decades, RA Power Solutions has led the industry in portable crankshaft grinding, enabling repair directly on vessels or in power plants—eliminating the need to dismantle or transport heavy engine components. RA Power Solutions manufactures the insitu crankshaft grinding machine, which is lightweight, portable, and easy to operate. We developed and manufactured this … Continue reading “Insitu Crankshaft Grinding Machine – RA Power Solutions”

High-Quality Cylinder Liners: Our Expertise & Offerings

At RA Power Solutions, we manufacture new and reconditioned cylinder liners for engines, compressors, generators, and rotating equipment worldwide. Our capacities and quality assurance stand out in the marine and diesel engine industry.

 We strictly follow the centrifugal process for casting cylinder liners. The material composition of cylinder liners is maintained strictly as per the manufacturer’s specifications.

Cylinder Liner of WARTSILA 12V46C
                 Cylinder Liner of WARTSILA 12V46C

Our Capabilities:

  • Lengths up to 1,500 mm and bores up to 600 mm
    We handle liners of heavy-duty dimensions to serve industrial and marine engines.
  • Centrifugal casting
    Using this robust process ensures dense, uniform castings free from blow-holes or porosity.
  • Machining & honing in-house
    A suite of CNC and precision honing machines lets us maintain tight tolerances and surface finish specs.
  • Rigorous quality inspections
    Each liner undergoes dimensional checks, MPI/crack detection, blow-hole inspections, and other metallurgical tests. We provide detailed inspection reports on request.
  • Manufactured to spec
    Whether based on drawings or client samples, we can develop and produce cylinder liners in small or bulk quantities.

Why Choose Our Cylinder Liners?

Features Benefits
Centrifugal casting Ensures dense, defect-free castings
Advanced machining and honing Maintains OEM-level tolerances and finishes
In-house quality control Guarantees inspection and metallurgical integrity
Flexible manufacturing Accepts drawings or samples, small-batch capability
Reconditioned liners available Cost-efective alternative with near-new performance
Cylinder Liners for Wartsila Diesel Engine
           Cylinder Liners for Wartsila Diesel Engine

We have  High Quality cylinder liners of the following makes in stock:

ABB, ABC, Anglo Belgian Corporation, Akasaka, Alco Diesel Engines, Alfa Laval, Allen, Alpha Diesel, Alstom, B & W, Bergen Diesel Engines, Blackstone, Bosch, Caterpillar, Cegielski,  Consilium, Crepelle, Cummins, Daihatsu, Detroit Diesel, Deutz, DeutzMarine Engine, EMD, Fiat, FUJI, Fuji Diesel, Furuno, Hanshin, Headway, HIMSEN, Holset, Hyundai, JRC, Kawasaki, Kelvin Hughes, Kongsberg Maritime, L’OrangeMaschinenfabrik, MaK, MAN, MAN B&W, Martek Marine, Mirrlees Blackstone, Mitsubishi, Mitsubishi UE/UEC, MTU, MWM, Napier, NAVTEX, Nigata, Nohab Diesel, Paxman, Pielstick, Ruston & Hornsby, Samsung, Simrad, SKL, Sperry, Stork SW Diesel, Stork Werkspoor, STORK-WARTSILA DIESEL, Sulzer, Volvo Penta, Wartsila, Wartsila Diesel, Westfalia,  Wichmann, Woodward, Yanmar, etc.

Cylinder Liner of Diesel Engine

For more information regarding High Quality Cylinder Liners, cylinder liner repair, email us at rajshahani@rapowersolutions.cominfo@rapowersolutions.com, or call us at +91 9582647131 or +91 9810012383.

FAQs:

Q1: What is a cylinder liner?

A replaceable sleeve inserted into an engine block to form the cylinder bore.

Q2: Why are cylinder liners used?

They improve wear resistance, enable engine overhauls, and extend engine life.

Q3: What’s the difference between dry and wet liners?

Dry liners don’t touch coolant; wet liners do and require sealing.

Q4: Are reconditioned cylinder liners reliable?

Yes, if refurbished to OEM specs, they perform like new at a lower cost.

Q5: What material is used for manufacturing liners?

High-grade alloy cast iron, often made using centrifugal casting.

At RA Power Solutions, we manufacture new and reconditioned cylinder liners for engines, compressors, generators, and rotating equipment worldwide. Our capacities and quality assurance stand out in the marine and diesel engine industry.  We strictly follow the centrifugal process for casting cylinder liners. The material composition of cylinder liners is maintained strictly as per the … Continue reading “High-Quality Cylinder Liners: Our Expertise & Offerings”

Metal Stitching and Thread Repair Inserts – RA Power Solutions

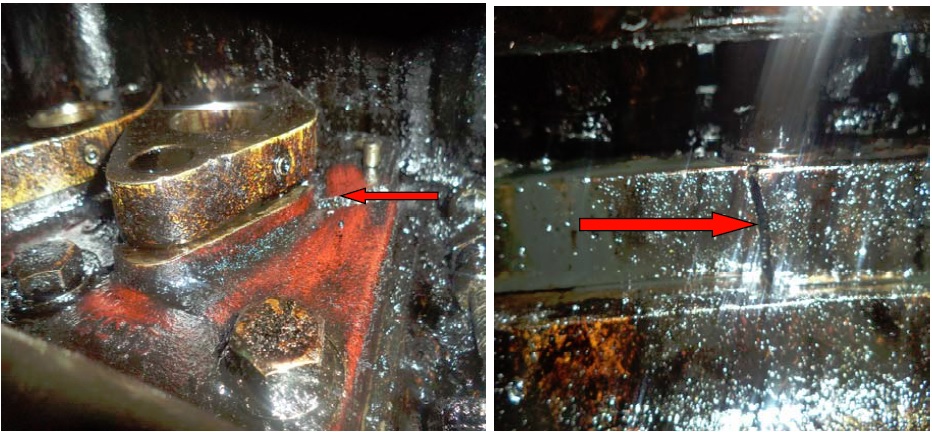
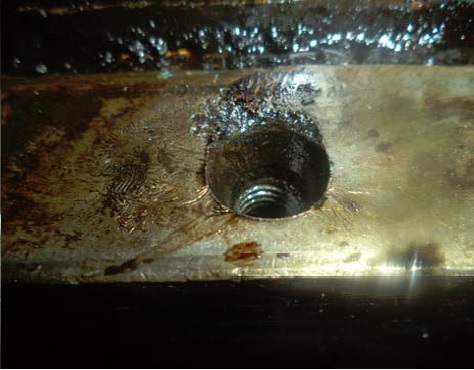
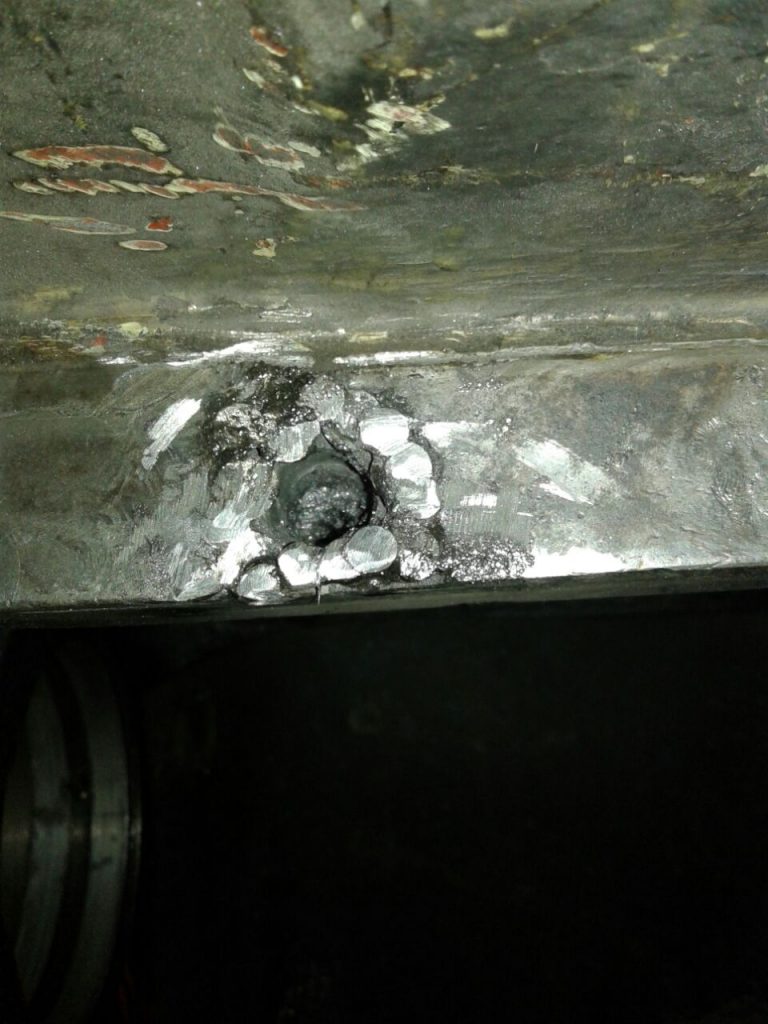
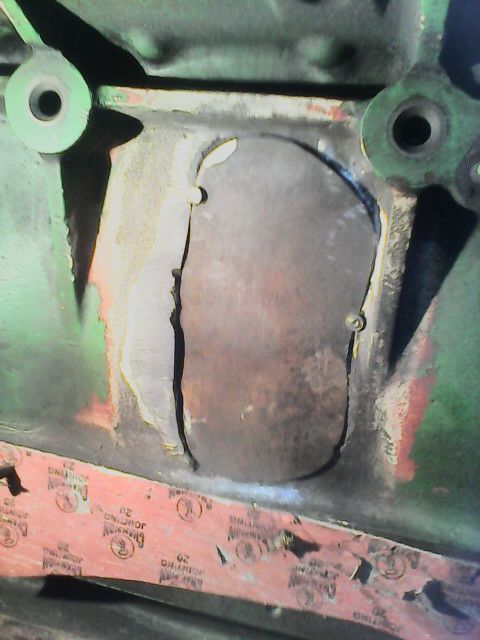
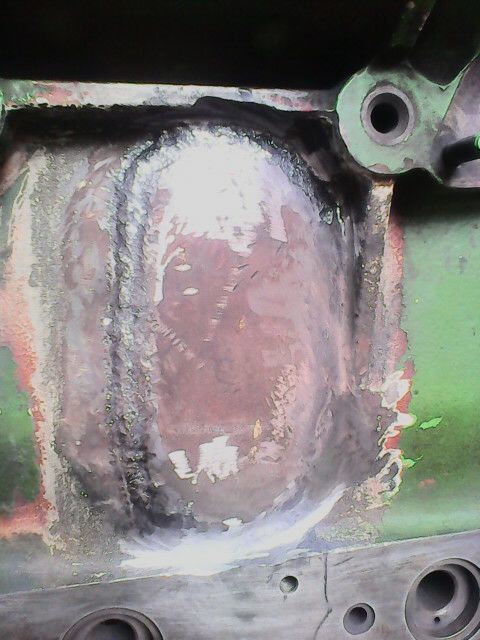
One of our clients informed RA Power Solutions about damage to the cam case cover of a MAN diesel engine on board a vessel sailing near China. After reviewing the details and photographs, we observed that the cam case cover had broken into pieces. We also found that the threads on the engine body and the dowel pin were damaged.

Cracked Housing of Engine Block
Broken Area
Broken Area
Damaged Upper Threads

RA Power Solutions Executes Onboard Repair of Engine Block and Cam Case Cover Sitting Area:

RA Power Solutions deputed their team of technicians on board the vessel, and they executed the repair of engine block, cam case cover sitting area by the following procedure:

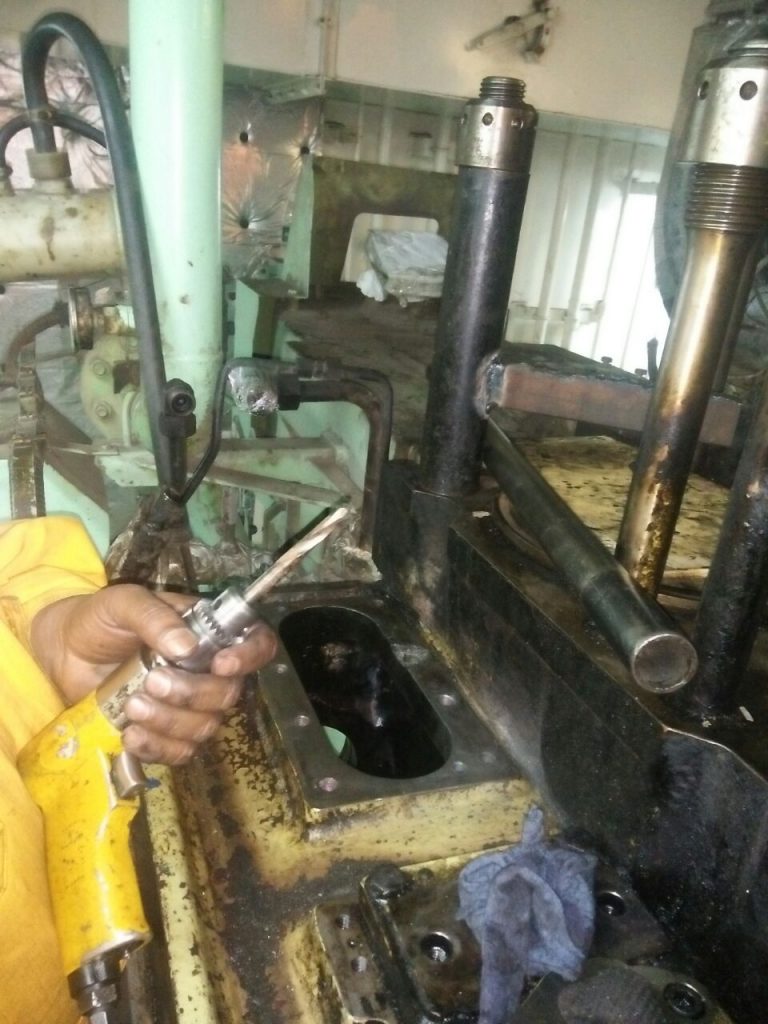
  • The broken bolt which remained inside the thread hole was drilled out.
  • The damaged threads on cam cover sitting area on entablature was removed by drilling new blind holes, suiting the new M12 Helicoil thread inserts.
  • Re-tap holes for the new M12 Helicoil thread inserts was done carefully.
  • New M12 Helicoil thread inserts were installed in the engine frame/ entablature.
  • The 2 guide pins for the roller guide housing were removed, taking due precaution.
  • Technicians installed a new roller guide housing using correct M12 hexagon bolts. They also included the newly introduced 10 mm washers.
  • Technicians completed the final alignment of the roller guide housing. They then tightened the bolts using the correct tightening torque.
  • Technicians drilled two ø8 mm guide pinholes in both the roller guide housing and the engine frame. Afterwards, they installed new guide pins.
repair of Threads on Engine Block Under Process
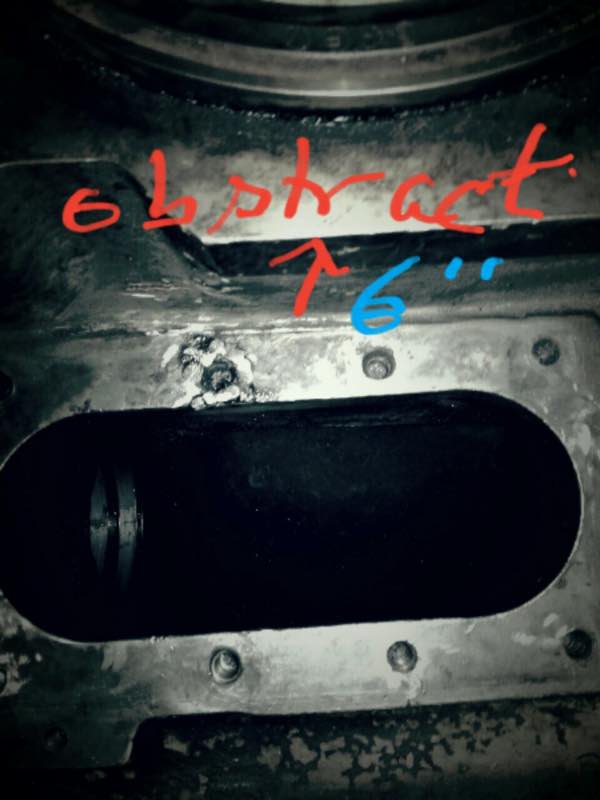
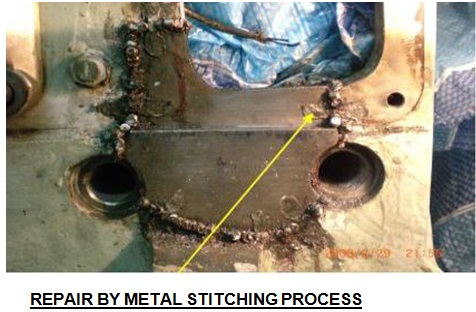
Repair of Thread Hole by Metal Stitching

What Is Metal Stitching?

Metal stitching, also known as metal locking, uses a cold repair technique to fix cracked or broken cast components. This method eliminates the need for welding. The process restores original strength and ensures pressure-tight sealing through mechanical locking of stitching pins and studs.

Advantages of Metal Stitching Over Welding:

  • No heat means no distortion, warping, or residual stress
  • Maintains alignment and surface profile of the original cast
  • Suitable for cast iron, steel, aluminum, and other alloys
  • Creates permanent, pressure- and liquid-tight repairs
  • Enables on-site repairs with minimal disassembly
  • Often stronger than the original material
Damaged Thread Hole Under Metal Stitching and Metal Locking
Metal Stitching of Bottom Area of Threaded Hole to Give Extra Strength

Our Process at RA Power Solutions:

  • Damage Inspection & Assessment: Document cracks and thread damage
  • Thread Repair via Stitching & Inserts: Use stitching keys and Helicoil/insert methods
  • Post-Repair Finishing: Grind and align to restore original surface
  • Testing & Validation: Conduct pressure or stress tests to ensure integrity.

With decades of experience and advanced cold-repair tools, RA Power Solutions delivers efficient and durable repairs without removing heavy castings.

Cam Cover Sitting Area of Engine Block After Repair

For more on metal stitching and metal locking, metal stitching of engine block contact us today email us at rajshahani@rapowersolutions.com, info@rapowersolutions.com, or call us at +91 9582647131 or +91 9810012383.

FAQs:

1. What is metal stitching, and how does it work?

Metal stitching, also known as cold metal locking, is a mechanical repair process used to fix cracks in cast iron or cast steel components. It involves inserting stitching pins and locks to restore structural integrity—without welding or heat.

2. When should I use thread repair inserts like Helicoil?

You should use thread repair inserts when original threads in an engine block, casing, or housing become stripped, worn out, or damaged. Helicoils restore the thread’s strength and allow secure fastening, even under high torque.

3. Is metal stitching better than welding for cast iron repair?

Yes. For cast iron and other brittle materials, metal stitching is safer and more reliable than welding. It avoids heat distortion, cracking, and structural weakening, which are common risks with welded repairs.

4. Can RA Power Solutions perform these repairs on-site?

Absolutely. RA Power Solutions specializes in on-site metal stitching and thread repair, including work on marine vessels, power plants, offshore rigs, and remote industrial sites—without the need to remove the equipment.

5. What components can be repaired using metal stitching and thread inserts?

These techniques can repair engine blocks, cylinder heads, gearboxes, cam case covers, pump casings, compressors, and more. These methods can typically restore any cracked or damaged cast iron or steel component.

One of our clients informed RA Power Solutions about damage to the cam case cover of a MAN diesel engine on board a vessel sailing near China. After reviewing the details and photographs, we observed that the cam case cover had broken into pieces. We also found that the threads on the engine body and … Continue reading “Metal Stitching and Thread Repair Inserts – RA Power Solutions”

Crankshaft Repair at Low Cost In Bangladesh- RA Power Solutions

Crankshaft repair is required in case of following observations:

I) Development of taper and ovality due to continuous running.

II) Seizure of bearing, increase in hardness, and development of crack.

III) Loss of alignment of the crankshaft or change in web deflection of crankshaft and many more reasons.

Damaged Crank Pin of MAN Diesel Engine

RA Power Solutions Pvt. Ltd. undertakes crankshaft repair in Bangladesh. We have a team of experienced technicians who undertake crankshaft repair onsite. These days, there is no need of remove the crankshaft from the Engine block and send it to the workshop for crankshaft repair.

Crack Detection of Crankpin Before Grinding

RA Power Solutions undertakes crankshaft repair, crankshaft grinding, and crankshaft polishing onsite without the removal of the crankshaft from the engine block. The onsite repair of crankshaft not only reduces the downtime but saves considerable costs in terms of removal of crankshaft, packing, transportation, etc. The sending of crankshaft to the workshop now is outdated.

Crankshaft Repair on Board the Vessel

RA Power Solutions have facility to undertake in situ crankshaft repair from 50 mm to 700 mm in diameter. Having more than 47+ years of experience, we have highly skilled in-house technicians to execute crankshaft repair. We are the most respected and cost-effective company in the Asian region. We also manufacture crankshaft repair machines and crankshaft grinding and polishing machine which is lightweight and easy to operate. 

Crankshaft Grinding of Damaged Crankpin on Board the Vessel

The range of machine is from 50 mm to 700 mm which is reasonably priced, and we have sold more than 63 machines all over the world. Author of this blog is Raj Shahani, Managing Director of RA Power Solutions Pvt. Ltd. having experience of more than 47+ years.

Crack Detection of Crankpin After Grinding

The company deals in onsite crankshaft grinding, crankshaft repair, rebabbitting of bearings, metal stitching/metal locking of cast iron, connecting rod repair, etc.

We have been regularly executing onsite crankshaft repair in Bangladesh, Madagascar, Oman, Qatar, Philippines, Bahrain, Sri Lanka, Myanmar, Turkey, Nigeria, Greece, Saudi Arabia, UK, Dubai, Malta, Cyprus, Singapore, Malaysia, Colombia, Iraq, Iran, Dubai, Antigua and Barbuda, Belize, Dominica, Dominican Republic, Netherlands, Belgium South America, Jordan, Ecuador, Singapore, Indonesia, Brazil, Scotland, Italy, UK, South Africa, etc.

Crankpin After Grinding

We also have engine crankpin bearings available in our stock for various engine models from Wärtsilä, MAN B&W, Sulzer, Yanmar, Daihatsu, MAK, Caterpillar, Cummins, Deutz, Mitsubishi, Allen, Himsen, and Niigata.

For more details, contact us at rajshahani@rapowersolutions.com or info@rapowersolutions.com, or call us at +91 9582647131 or +91 9810012383 for more information.

FAQ

1. What is in situ crankshaft grinding?
In situ crankshaft grinding is a method for repairing a damaged crankshaft without removing it from the engine.

2. What are the benefits of onsite crankshaft repair? 
On-site repair of the crankshaft not only saves time and reduces the cost of repairs but also ensures that the part does not need to be taken to a workshop for repairs.

3. Why is onsite crankshaft repair preferred?
Onsite crankshaft repair saves time and money by repairing the crankshaft without removing it from the engine.

4. Do you provide crankshaft repair services in Bangladesh?
Yes. RA Power Solutions offers services of in-situ crankshaft grinding, crankpin polishing, and crankshaft repairing in Bangladesh. Our engineers will visit your site and perform the services.

Crankshaft repair is required in case of following observations: I) Development of taper and ovality due to continuous running. II) Seizure of bearing, increase in hardness, and development of crack. III) Loss of alignment of the crankshaft or change in web deflection of crankshaft and many more reasons. RA Power Solutions Pvt. Ltd. undertakes crankshaft … Continue reading “Crankshaft Repair at Low Cost In Bangladesh- RA Power Solutions”

Connecting Rod for Sale – RA Power Solutions

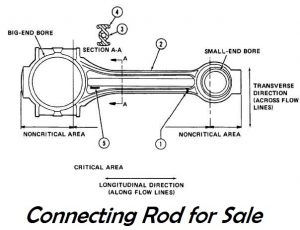
Connecting Rod for Sale

We maintain a large stock of reconditioned connecting rods and new connecting rods of the following makes of diesel engines:

MAIN & AUX. ENGINES

MAN-B&W Sulzer Wartsila
MAK Deutz Pielstick
Mitsubishi Daihatsu Yanmar
Bergen Niigata Himsen
Fiat Allen Hanshin
MWM Caterpillar SKL
Ruston Crepelle Stork
Paxman Mirrlees Blackstone Alco, ABC, Crepelle, Nohab, etc.

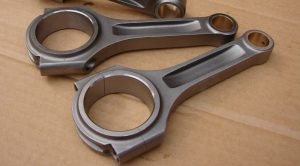
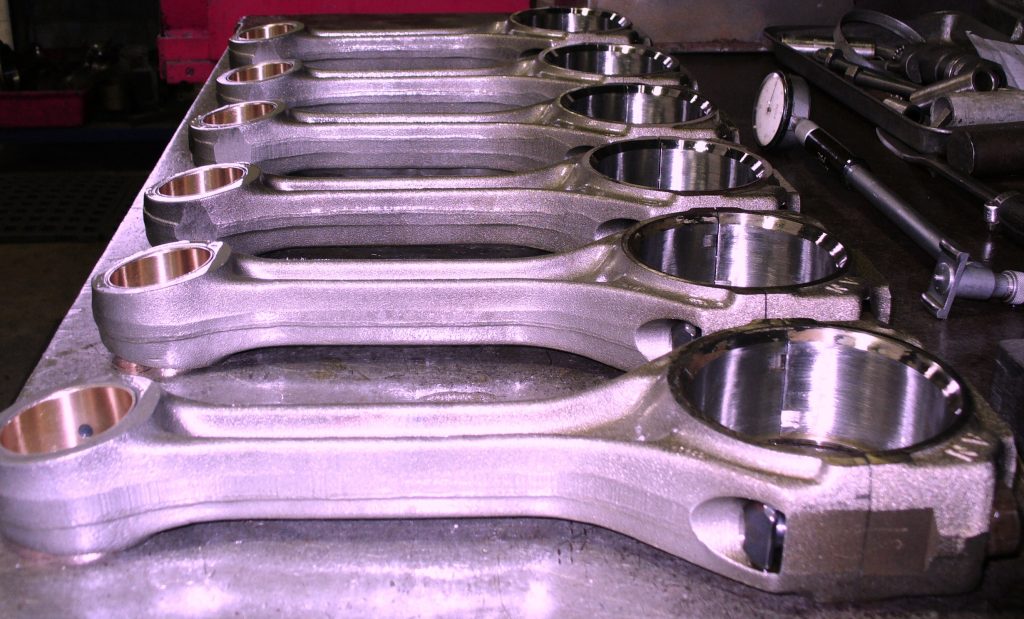
Connecting Rod of Daihatsu Diesel Engine

Each connecting rod is passed through stringent quality control procedures by the technicians having more than 47+ years of experience. In case of any deviation, connecting rods are repaired in-house on the latest breed of special purpose machine.

Connecting Rod of MAK Diesel Engine for Sale

The big end of the connecting rod is re-bored and standard bore tolerance as specified in the manual is maintained. In case of small end, the bush is replaced by new one and re-bored to the standard size. Each connecting rod is subject to dimensional inspection and passes through the crack detection test by MPI. We don’t recommend repair of bend connecting rod or the connecting rods which has lost its alignment/straightness.

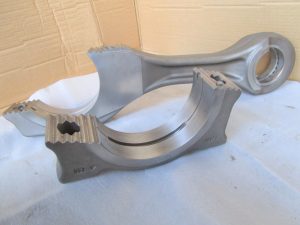
Connecting Rod Under Reconditioning

The connecting rods supplied are 1/3rd the cost of new connecting rod resulting to the huge saving for the owners. For more information regarding engine connecting rods, crankshaft reconditioning, connecting rod replacement, marine engine spares, bearings for Yanmar engine, maintenance and repair services, and engine overhaul services email us at: rajshahani@rapowersolutions.com or info@rapowersolutions.com, or call us at +91 9582647131 or +91 9810012383.

Inspection of Wartsila Connecting Rod

FAQ

1. What types of connecting rods do you offer?
RA Power Solutions provides new and remanufactured connecting rods for marine, diesel, and industrial engines. We have parts for the main engine builders, including MAN B&W, Wärtsilä, Sulzer, MAK, Daihatsu, Yanmar, Caterpillar, Mitsubishi, Deutz, Bergen, and many more.

2. How are reconditioned connecting rods inspected?
Every remanufactured connecting rod is subject to a comprehensive quality inspection. The big end is bored out to standard specification, the small end bush is replaced and machined to the correct size, and the connecting rod is checked for dimensions and tested for cracks using MPI (magnetic particle inspection).

3. Do you repair damaged connecting rods?
Yes, RA Power Solutions fixes connecting rods with minor wear or damage. We don’t advocate correcting bent or misaligned connecting rods, though, as this could compromise engine performance and reliability.


We maintain a large stock of reconditioned connecting rods and new connecting rods of the following makes of diesel engines: MAIN & AUX. ENGINES MAN-B&W Sulzer Wartsila MAK Deutz Pielstick Mitsubishi Daihatsu Yanmar Bergen Niigata Himsen Fiat Allen Hanshin MWM Caterpillar SKL Ruston Crepelle Stork Paxman Mirrlees Blackstone Alco, ABC, Crepelle, Nohab, etc. Each connecting … Continue reading “Connecting Rod for Sale – RA Power Solutions”

Portable Crankshaft Polishing Machine – RA Power Solutions

 In case of bearing failure or continuous running of the crankshaft, it develops bearing line marks, pitting, or rough surfaces. This requires polishing of the crankshaft, crankpin, and main journal.

A revolutionary in situ portable crankshaft polishing machine has been introduced by RA Power Solutions Pvt. Ltd., which is portable, lightweight, easy to operate, and can be taken to the site. The polishing of the crankshaft and crankpin is possible without removing the crankshaft from the engine block. We manufacture the onsite crankshaft polishing machine for diameters ranging from 50 mm to 700 mm.

The use of a crankshaft polishing machine removes bearing line marks and pitting. It also improves the surface finish as required by the manufacturer.

Crankshaft Polishing Machine Packed in Steel Box

We provide free training to customers for a duration of one week. During this time, our team explains and demonstrates the operation and maintenance of the crankshaft polishing machine.

The cost of the machine is kept low, as it is the company’s objective that nobody should spend an exorbitant amount on polishing and grinding the crankshaft anymore, and sending it to the workshop. More than 60 machines are sold all over the world.

Close-Up View of Crankshaft Polishing Machine After Packing
 
Packing in Progress Insitu Crankshaft Grinding Machine

Our team developed the crankshaft grinding and polishing machine through consistent and focused R&D. We also conducted field trials under various operating conditions.

The company aims to reduce the cost of repairing crankshafts. It also seeks to eliminate the outdated practice of sending crankshafts to workshops. For more information on crankshaft polisher, crankshaft polisher machine, crankshaft polishing tool, crankshaft polisher for sale, polishing crankshaft journals, crankshaft polishing, crankshaft grinding machine, and crankshaft polishing equipment — contact us at rajshahani@rapowersolutions.com or info@rapowersolutions.comCall: +91 9582647131 / +91 9810012383

We also have engine crankpin bearings available in our stock for various engine models from Wärtsilä, MAN B&W, Sulzer, Yanmar, Daihatsu, MAK, Caterpillar, Cummins, Deutz, Mitsubishi, Allen, Himsen, and Niigata.

FAQs:

1. Can the crankshaft be repaired without removing it from the engine?

Yes, RA Power Solutions designed the in-situ crankshaft polishing machine to operate directly inside the engine block through the inspection window. The process eliminates the need to remove the crankshaft. This approach saves both time and cost.

2. How long does it take to repair a crankpin or main journal?

Typically, technicians complete a full in-situ repair—including inspection, setup, grinding, and final polishing—within 24 to 30 hours. The exact time depends on the extent of the damage.

3. What types of engines can this machine be used on?

The portable crankshaft polishing machine is suitable for marine engines, power plant generators, compressors, diesel locomotives, construction equipment, and mining machinery. It is also ideal for other heavy-duty engines. The machine works effectively for both land-based and shipboard applications.

4. What is the diameter range this machine can handle?

The portable polishing machine can service crankshafts with a diameter range from 35 mm to 700 mm. Custom solutions are available for crankshafts up to 1000 mm in diameter.

5. How precise is the machine in terms of finish and tolerance?

The machine achieves a surface finish as fine as 0.15–0.2 µm Ra and maintains dimensional tolerances within 0.01 to 0.025 mm, meeting or exceeding OEM standards.

 In case of bearing failure or continuous running of the crankshaft, it develops bearing line marks, pitting, or rough surfaces. This requires polishing of the crankshaft, crankpin, and main journal. A revolutionary in situ portable crankshaft polishing machine has been introduced by RA Power Solutions Pvt. Ltd., which is portable, lightweight, easy to operate, and … Continue reading “Portable Crankshaft Polishing Machine – RA Power Solutions”
Connecting Rod Reconditioning for Marine & Diesel Engines

At RA Power Solutions, we understand that connecting rods endure immense operational stresses—from rapid acceleration and deceleration to reciprocating motion and high rpm. Over time, wear and tear can lead to taper and ovality, misalignment, and even micro-cracks in rods and bolts.

Why Connecting Rod Reconditioning Matters?

  • High-pressure environment: The connecting rod sustains piston weight, combustion shock loads, and high rpm—making accurate alignment and dimensional integrity essential.
  • Common defects: Big and small end taper or ovality, loss of centerline alignment, and fatigue-related bolt cracks. These issues affect efficiency and can lead to costly engine failure.
Connecting Rod Assembled with Piston after Repair

Coverage Across Multiple Engine Brands

With over 47+ years of expertise, RA Power Solutions reconditions connecting rods for all major marine and industrial diesel engines, including: MAN‑B&W, Sulzer, Wärtsilä, Mak, Deutz, Pielstick, Mitsubishi, Daihatsu, Yanmar, Bergen, Niigata, Caterpillar, Paxman, Crepelle, and many more.

We also stock a vast inventory of reconditioned rods—pricings typically one-third of new OEM parts, offering substantial savings without compromising quality.

Key Benefits at a Glance

FeatureBenefit
Comprehensive testingMPI crack detection ensures safety
Accurate machiningMaintains precision tolerances
OEM-level certificationQuality assurance with calibration reports
Significant cost savingsUp to ~66% cheaper than new rods
Large inventory coverageSupport for dozens of engine makes/models

Following steps are followed for reconditioning and resizing of connecting rod

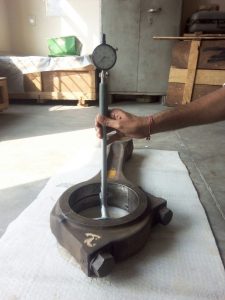
  • We check the connecting rod for parallelism and alignment. We also inspect the big end and small end for taper and ovality.
  • RA Power Solutions Pvt. Ltd. recommends not repairing connecting rods that are bent, based on their experience.
  • We perform crack detection by MPI on the bolt seating area and bolts during connecting rod reconditioning.
  • The connecting rod bolts are under heavy stress all the time and develop hairline cracks. It is recommended to replace connecting rod bolts after certain hours of operation as specified in the manual.
  • We re-bore the connecting rod big end to the standard size and maintain the required tolerances. For the small end, we recommend replacing the bush and re-boring it while ensuring the center distance between the big end and small end bores matches the manufacturer’s specifications..
Connecting Rod of Yanmar Ready for Dispatch
Reconditioning of Connecting Rod

Ready to Retrofit Your Engine with Reconditioned Connecting Rods?

Boost engine reliability and slash maintenance costs with precision-engineered, certifiable connecting rod reconditioning. We’re here to support your marine, industrial, or power generation needs with global reach and expert execution.

Connecting Rod Reconditioning
Connecting Rod of Diahatsu Marine Diesel Engine

We also have engine crankpin bearings available in our stock for various engine models from Wärtsilä, MAN B&W, Sulzer, Yanmar, Daihatsu, MAK, Caterpillar, Cummins, Deutz, Mitsubishi, Allen, Himsen, and Niigata.

For more information regarding Connecting Rod Reconditioning, Connecting Rod for marine engine. Contact us at rajshahani@rapowersolutions.com or info@rapowersolutions.com, or call us at +91 9582647131 or +91 9810012383.

Q1: What is connecting rod reconditioning?

Connecting rod reconditioning is the process of restoring worn or damaged connecting rods to their original specifications. It includes checking for cracks, re-boring the big and small ends, replacing bushes, and ensuring alignment and correct center-to-center distance.

Q2: When should a connecting rod be reconditioned?

Reconditioning is recommended when there is excessive ovality or taper in the big or small end bores, loss of alignment, visible wear, or damage caused by overheating or improper lubrication.

Q3: Can all connecting rods be reconditioned?

No. If the connecting rod is bent or has deep cracks (especially around the bolt seating area), it is not recommended for repair. We evaluate each rod individually using MPI and dimensional checks.

Q4: What is the importance of replacing the bush in the small end?

The bush ensures the correct fit and function of the piston pin. Replacing and re-boring the bush helps maintain proper clearance and ensures the center distance between the big and small end is within OEM specifications.

Q5: What testing methods are used during reconditioning?

We use Magnetic Particle Inspection (MPI) to detect surface cracks. Dimensional checks are performed for parallelism, taper, ovality, and alignment. Final measurements are verified against manufacturer tolerances.

At RA Power Solutions, we understand that connecting rods endure immense operational stresses—from rapid acceleration and deceleration to reciprocating motion and high rpm. Over time, wear and tear can lead to taper and ovality, misalignment, and even micro-cracks in rods and bolts. Why Connecting Rod Reconditioning Matters? Coverage Across Multiple Engine Brands With over 47+ … Continue reading “Connecting Rod Reconditioning for Marine & Diesel Engines”

Heat Exchanger Gaskets – RA Power Solutions

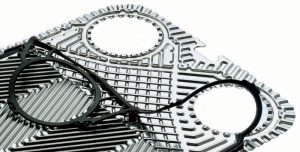
Heat Exchanger Gaskets are important for satisfactory performance of the main equipment. We manufacture gaskets for all makes and equipments where gaskets are used.

Plate Heat Exchanger Gaskets

For more than 47+ years, we have been specializing in manufacturing of precision rubber gaskets as per the manufacturer’s requirement. The rubber gaskets of all types like Neoprene gaskets, silicone gasket, Viton gasket, EPDM gasket, nitrile gasket are manufactured.

Heat Exchanger Gaskets

RA Power Solutions Pvt. Ltd. manufactures plate heat exchanger gaskets in accordance with a thorough quality control process. We fully inspect gaskets to ensure that they meet international standards with the help of our gaskets testing facilities.

Gasket
Gasket

We also have engine crankpin bearings available in our stock for various engine models from Wärtsilä, MAN B&W, Sulzer, Yanmar, Daihatsu, MAK, Caterpillar, Cummins, Deutz, Mitsubishi, Allen, Himsen, and Niigata.

We offer a 12-month warranty for all plate heat exchanger gaskets supplied by us. Contact us at rajshahani@rapowersolutions.com or info@rapowersolutions.com, or call us at +91 9582647131 or +91 9810012383.

FAQs

1. What are heat exchanger gaskets used for?
Heat exchanger gaskets help to form a seal between the plates, avoiding any leakage problems.

2. What types of heat exchanger gaskets are available?
We provide heat exchanger gaskets in Neoprene, EPDM, Nitrile, Silicone and Viton for various operating situations.

3. How are heat exchanger gaskets tested?
All gaskets are subjected to a rigorous quality control process, including inspection and testing, to ensure they satisfy international quality requirements.

4. What are the benefits of high-quality heat exchanger gaskets?
High-quality heat exchanger gaskets give a leakproof seal, increase the efficiency of machinery, minimize costs, and improve the life span of the heat exchanger.

Heat Exchanger Gaskets are important for satisfactory performance of the main equipment. We manufacture gaskets for all makes and equipments where gaskets are used. For more than 47+ years, we have been specializing in manufacturing of precision rubber gaskets as per the manufacturer’s requirement. The rubber gaskets of all types like Neoprene gaskets, silicone gasket, … Continue reading “Heat Exchanger Gaskets – RA Power Solutions”
Crankshaft Repair While Sailing – RA Power Solutions

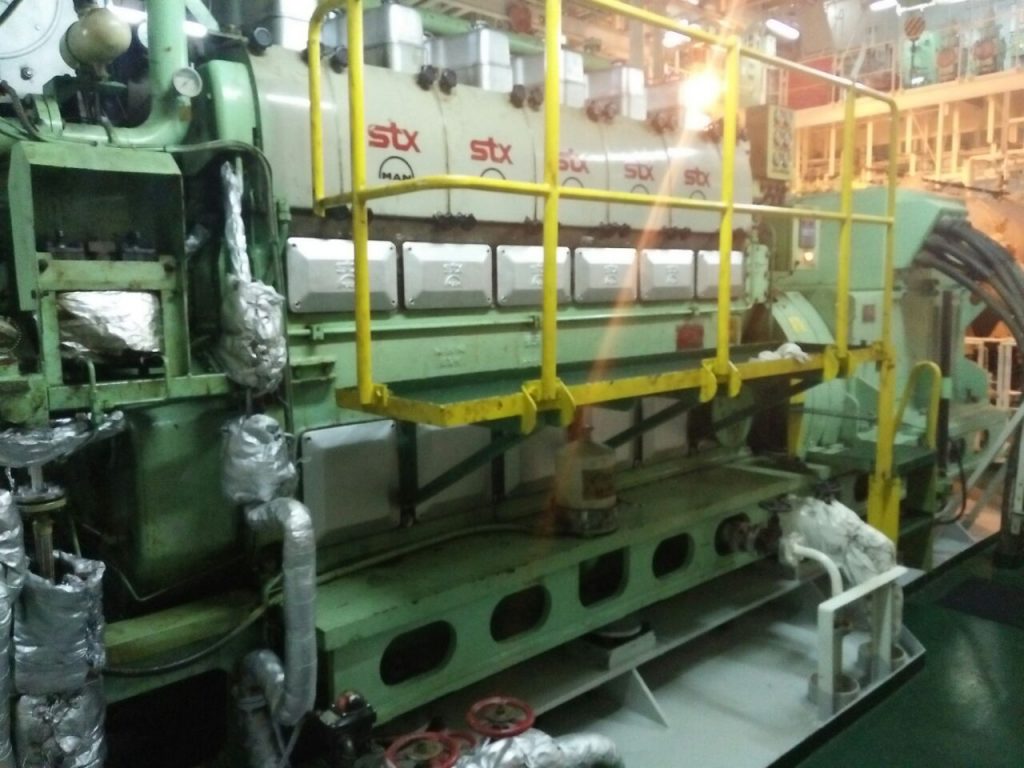
RA Power Solutions is the first company to offer crankshaft grinding and polishing services while a vessel is sailing, using onboard, vibration-free portable equipment. This enables precision repairs without removing the crankshaft from the engine block, saving valuable time and reducing costs.

MAN B&W STX 6L23/30H

Case Study: MAN 6L32/40 Repair at Sea

  • Engine Model: MAN 6L 32/40, crankpin diameter 290 mm, bearing width 130 mm
  • Vessel sailed from Savannah (USA) to Panama during repair
  • All six crankpins showed excessive ovality (0.10–0.25 mm), well above the 0.03 mm tolerance
  • Hardness tests fell within acceptable limits; MPI crack checks revealed no anomalies
  • Technicians ground five pins by 0.5 mm and one by 2.0 mm due to localized damage
  • Post-repair, RA Power specialists assisted ship’s crew with connecting rod calibration
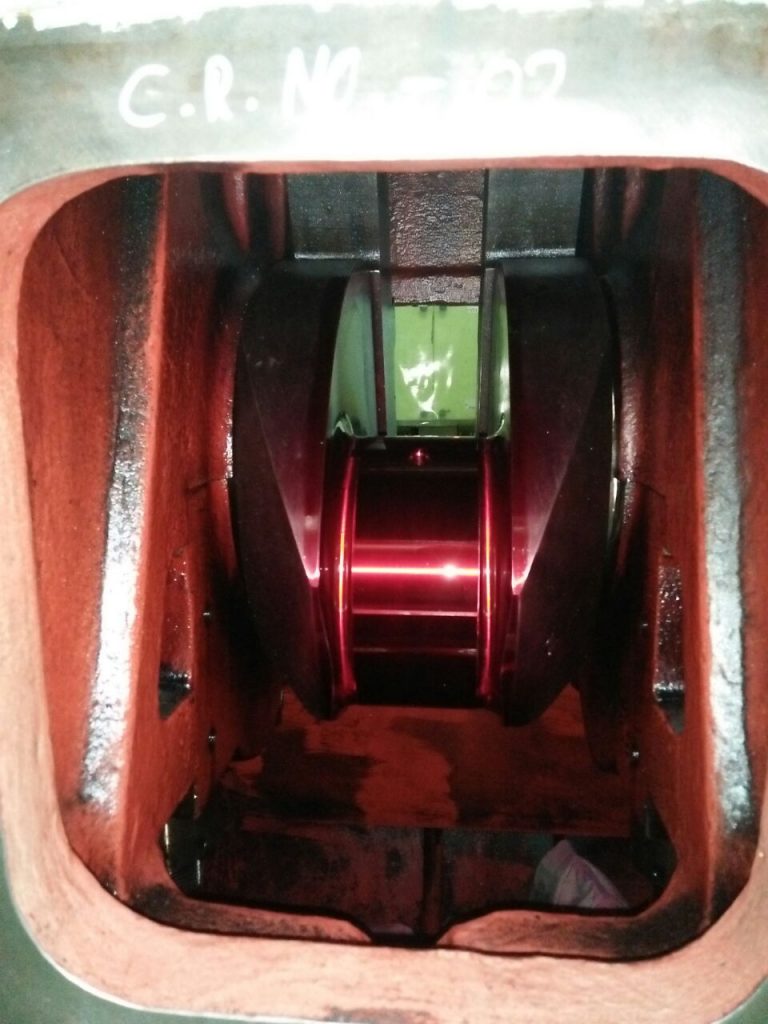
Crankpin Under Grinding Process
Crankshaft Polishing is in Process

Advantages of RA Power’s Onboard Crankshaft Repair

  • Utilizes latest-design portable grinding equipment, capable of close-tolerance machining. 
  • Enables crankshaft repair during sailing, minimizing vessel downtime and eliminating overhaul costs.
  • Offers 24/7 emergency service—technicians have valid seaman documentation and US visas for rapid deployment.
  • Provides practical, experienced advice based on nearly five decades in in situ crankshaft repair, avoiding rejection or replacement.
  • Repairs damaged radius fillets and journals at no extra cost, offering one of the lowest-cost solutions in the industry .
Crankpin Under Test to Check Crack
Dye Penetrant Test of Crankpin

Why Choose RA Power Solutions?

  • Speed & efficiency: finish inspections and repairs onboard in under 48 hours.
  • Lower costs: no need for crane lifts, dry docking, or workshop transport.
  • Precision & reliability: strict adherence to manufacturer tolerances.
  • 24/7 availability: emergency interventions worldwide with minimal lead time.
  • Decades of trust: thousands of crankshafts repaired successfully across multiple continents .
Crankpin Ready After Grinding and Polishing

We also have engine crankpin bearings available in our stock for various engine models from Wärtsilä, MAN B&W, Sulzer, Yanmar, Daihatsu, MAK, Caterpillar, Cummins, Deutz, Mitsubishi, Allen, Himsen, and Niigata. 

For more information about our services for grinding of crankshaft, crankshaft grinding and polishing services, crankshaft repair, and restoring crankshaft of compressor, please email us at rajshahani@rapowersolutions.com or info@rapowersolutions.com, or call us at +91 9582647131 or +91 9810012383.

FAQs

1. Can a crankshaft be repaired while a vessel is sailing? 
Yes, crankshaft grinding and polishing can be done under sail with portable vibration-free equipment. Crankpins and journals that are worn or damaged can be repaired without removing the crankshaft from the engine block or putting the vessel in dry dock.

2. What are the benefits of crankshaft repair while sailing? 
Big pluses are less time in the yard, lower repair costs, and no need for dry docking or crane lifting. Depending on working conditions and safety requirements, the crankshaft can be inspected, ground, polished, and restored on board the vessel in her voyage.

3. Can ovality and localized crankpin damage be repaired onboard? 
Yeah. Excessive crankpin ovality, wear, scoring, and localized damage can often be rectified by precision grinding. The crankpin is checked for hardness, cracks, and manufacturer tolerances. This determines how much material needs to be removed.

4. How long does onboard crankshaft grinding and polishing take? 
Depending on the number of crankpins, extent of damage, required undersize, and accessibility, the inspection and repair can often be completed within 48 hours. Emergency crankshaft repairs are available while the vessel is underway.

5. Is crack detection performed before crankshaft grinding? 
Yes. Crankpins and journals should be checked for cracks before and after machining. Magnetic particle inspection (MPI) or dye penetrant testing can be performed depending upon the material of the crankshaft and the requirements for inspection. Hardness testing and dimensional measurements are also done to ensure that the crankshaft is within acceptable limits.

RA Power Solutions is the first company to offer crankshaft grinding and polishing services while a vessel is sailing, using onboard, vibration-free portable equipment. This enables precision repairs without removing the crankshaft from the engine block, saving valuable time and reducing costs. Case Study: MAN 6L32/40 Repair at Sea Advantages of RA Power’s Onboard Crankshaft … Continue reading “Crankshaft Repair While Sailing – RA Power Solutions”
Cast Iron Crack Repair with Metal Stitching & Metal Locking

Experts highly recommend metal stitching and metal locking for repairing cracks in cast iron. Industries around the world use this cold repair technique because it delivers reliable and effective results when restoring cast iron components.

Broken cast iron pieces can also be replaced by a new piece of casting undertaking metal locking. This technology is as old as the introduction of cast iron casting in industry.

Insertion of Casting Piece in Engine Block
Metal Stitching of Jenbacher Engine Block in Process

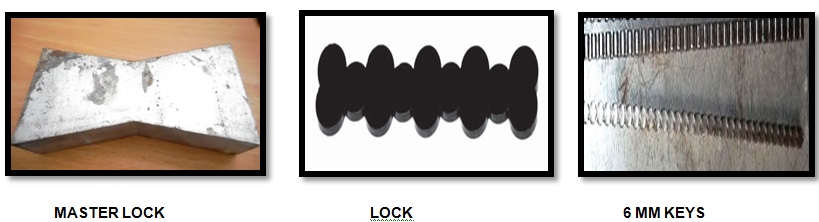
Metal keys and metal locks are used to undertake crack repair in cast iron casting.

Metal keys and Metal Locks are used in Metal Stitching/Locking Process

RA Power Solutions Pvt. Ltd. has a team of trained technicians who carry out metal stitching of broken or cracked castings directly onsite. They bring all necessary tools, consumables, and, if needed, a replacement casting to the site. The team repairs the crack onsite and avoids any need to disassemble or transport the equipment.

Metal Stitching Done in Broken Area of Generator

Tests and experience show that metal stitching repairs can strengthen cracked castings. The repaired section often becomes even more durable after the process. We execute crack repairs on board the vessel, in power plants all over the world.

Why Choose Cold Repair Over Welding?

Traditional welding uses heat to damage alignment, change grain structure, and weaken cast iron components. Cold repair procedures such as metal stitching and locking maintain the original material integrity. This results in stress-free, distortion-free, and high-strength solutions.

What Is Metal Stitching & Metal Locking?

Metal stitching is a cold bolt-locking process that includes drilling precise holes along a crack and inserting metal “keys” and studs into a dovetailed pattern. These studs bite into one another, tightening the crack and restoring structural rigidity.
Metal locking supports stitched joints with custom-shaped metal inserts, inhibiting additional proliferation and boosting long-term endurance.

We extend metal stitching services all over the world, including countries like Madagascar, Oman, Qatar, Philippines, Bahrain, Srilanka, Bangladesh, Myanmar, Turkey, Nigeria, Greece, Saudi Arabia, UK, Dubai, Singapore, Malta, and Cyprus, etc.

For more information on crack repair by metal stitching, Cast Iron Crack Repair, cast iron stitching, repair cast iron, cast iron metal stitching services, crack repair in cast iron, and repairing cast iron metal lock, contact us at rajshahani@rapowersolutions.com or info@rapowersolutions.com or call us at +91 9582647131, or +91 9810012383.

FAQs:

1. What is metal stitching in cast iron repair?

Metal stitching is a cold repair process used to restore cracked or damaged cast iron components. It involves inserting special metal keys and locking pins across the crack to mechanically join and seal it—without using heat or welding.

2. How is metal locking different from metal stitching?

While both methods are used together, metal locking adds reinforcement by embedding strong metal locks or inserts that cross the crack. These locks increase structural integrity and prevent further crack propagation.

3. Why is metal stitching better than welding for cast iron?

Welding applies heat that can distort the casting and cause new cracks due to thermal stress. In contrast, metal stitching is a cold process, meaning there’s no heat, no distortion, and the original metallurgical properties remain intact.

Experts highly recommend metal stitching and metal locking for repairing cracks in cast iron. Industries around the world use this cold repair technique because it delivers reliable and effective results when restoring cast iron components. Broken cast iron pieces can also be replaced by a new piece of casting undertaking metal locking. This technology is … Continue reading “Cast Iron Crack Repair with Metal Stitching & Metal Locking”